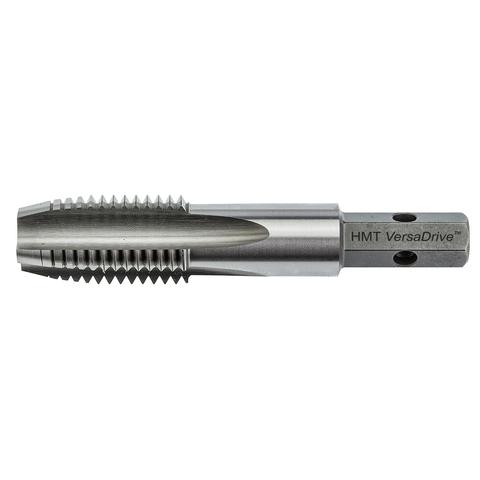

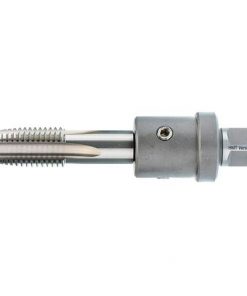
VersaDrive™ ImpactaTaps For Galvanised Bolts M16x2(+.15″)
£80.35 inc VAT
15X Faster than Hand Tapping
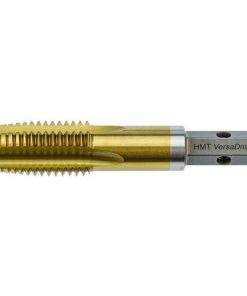
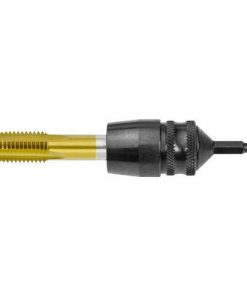
VersaDrive™ ImpactaTaps for Galvanised Bolts have an oversized thread to compensate for the increased thickness of coating found on galvanised steel fabrications or galvanised fixings.
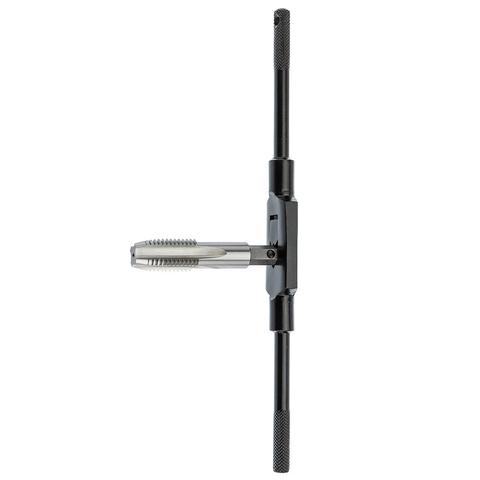
VersaDrive™ ImpactaTaps perform best when adapted for use with an Impact wrench for through holes. However, they can also be adapted for use in a reversible Magnet Drill, or even used with any standard Hand Tap wrench.
- Fast Tapping with Minimal Kickback; Specially hardened for Impact Wrench use
- Chipbreaker action for Automatic chip clearance when Impact Tapping
- Unique Dual-Point Starting Angle for easy alignment and fast cut
- High Grade Tool Steel with Ground Flutes for high accuracy & long life
- High Strength, Non-slip Shank Design
Galv Taps have an oversized thread to compensate for the increased thickness of coating found on galvanized steel fabrications or galvanised fixings.
1. Best Practice Advice – How to get the best out of your 308020 Oversized ImpactaTaps
- 308020 ImpactaTaps are recommended for through hole applications only.
- Pilot drill the exact tapping size hole for best results
- Select the correct torque power for impact wrench/drivers using the data range in the Torque / RPM guide below. If exact match is not available select the closest torque setting above the recommendation.
- Apply firm, steady feed pressure throughout the cut
- Ensure the Tap is inserted squarely to the hole – poorly aligned or off-centre taps will greatly increase the risk of breakage.
- When using cordless tools, consider that the torque may drop once the battery charge becomes low. Keep batteries well charged. Low battery charge can lead to lower torque which can break or damage taps as point 3.
- Ensure regular application of quality cooling lubricant, especially when drilling thick or hardened materials.
- Hardened or heat-affected materials may require higher torque, reduced RPM and feed rates and extra coolant
- Flame cut/punched holes will require more torque to tap than drilled holes due to heat build up. Caution: Sometimes flame cut holes do not have parallel sides meaning risk of tap breakage.
- Tap the hole in one pass where possible, applying adequate lubrication before you start.
- If the tap is over-run from the hole once it is tapped, to remove the risk of cross-threading/damage to the tap, remove the tap from the adapter and locate it in the thread by hand, before reversing.
- When re-threading an existing thread, use caution to avoid cross-threading which can lead to tap breakage or thread damage. It is advisable to insert/start the tap into the thread by hand before driving it through at the correct torque
| brand | Holemaker |
|---|
Related products
Holemaker Technology
Holemaker Technology
Holemaker Technology
Holemaker Technology
Holemaker Technology
Holemaker Technology
Holemaker Technology
Holemaker Technology
VersaDrive™ ImpactaTaps – Standard Metric Coarse Thread M30x3.5mm